Engineered for extreme wear resistance, micro-arc accuracy, and continuous heavy-duty operational efficiency.
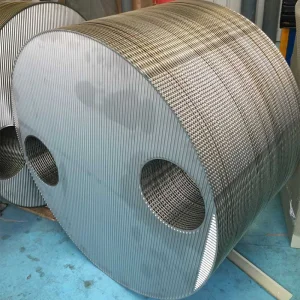
An Executive Strategic Analysis of Metallurgical Hardfacing, Thermal Dynamics, and Smart Factory Automation
The industrial sector in Grenville has undergone a massive technological shift. Historically anchored by structural fabrication, valve manufacturing, agricultural implement rebuilding, and heavy equipment maintenance, local enterprises are transitioning away from manual Gas Tungsten Arc Welding (GTAW/TIG) toward high-efficiency Plasma Transferred Arc (PTA) cladding and automated laser surfacing techniques.
As operating environments in regional sectors—such as petrochemical refinement, aerospace component servicing, and heavy earthmoving—become increasingly harsh, mechanical components face severe abrasion, chemical erosion, oxidation, and high thermal stress. Local workshops and plant operators in Grenville are rapidly upgrading to computerized plasma arc equipment to extend component operational lifespans by up to 300% to 500%.
Traditional welding methods like Submerged Arc Welding (SAW) or basic MIG hardfacing introduce high heat input into workpieces. This heat surge causes micro-cracking, structural distortion, and excessive substrate dilution (often exceeding 15% to 25%).
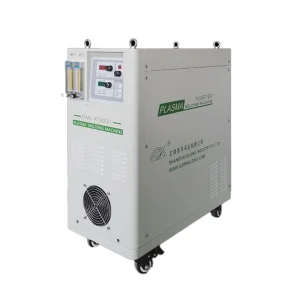
In contrast, Plasma Transferred Arc (PTA) technology offers a highly constricted, extremely stable energy beam. By utilizing a secondary pilot arc inside the plasma torch, gas is ionized into thermal plasma reaching temperatures upwards of 15,000°C to 20,000°C. This allows for precise control over dilution rates (maintained strictly under 5%), minimal Heat-Affected Zones (HAZ), and defect-free deposition of advanced alloys such as Stellite, Inconel, Hastelloy, and Cobalt/Nickel-based tungsten carbide matrices.
Arc Constriction Dynamics: Unlike unconstrained TIG arcs which expand outward, plasma arc torches force argon shielding gas through a tungsten electrode encased inside a water-cooled copper orifice. This mechanical constriction accelerates the gas flow into a high-density thermal jet.
Alloy Powder Feed Optimization: PTA surfacing feeds metal powders (ranging from 50 to 150 microns) directly into the plasma arc stream. The powder melts before entering the weld pool, securing a metallurgical bond with zero porosity and vastly superior wear characteristics compared to wire-fed systems.
| Process Parameter | Plasma Transferred Arc (PTA) | Laser Cladding System | TIG (GTAW) Hardfacing | Submerged Arc (SAW) |
|---|---|---|---|---|
| Base Metal Dilution Rate | Ultra-Low (3% – 5%) | Minimal (1% – 3%) | Moderate (10% – 15%) | High (20% – 30%) |
| Deposition Rate (kg/hr) | High (2.0 – 9.0 kg/h) | Medium (0.5 – 3.0 kg/h) | Low (0.5 – 1.5 kg/h) | Very High (> 10 kg/h) |
| Heat Affected Zone (HAZ) | Narrow & Controlled | Extremely Narrow | Wide | Extremely Wide |
| Consumable Versatility | Spherical Metal Powders | Laser Powder / Fine Wire | Solid / Cored Wires | Flux & Heavy Wires |
| Equipment ROI & Maintenance | Optimal / High Efficiency | High Capital Investment | Low Initial / High Labor | Moderate Initial Cost |
How Modern OEM Manufacturing Elevates Global Procurement Standards for Automated Industrial Welding Systems
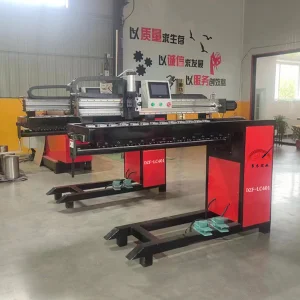
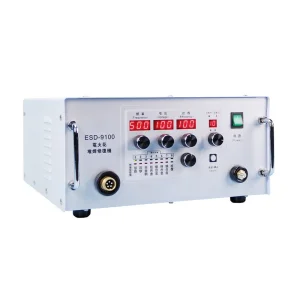
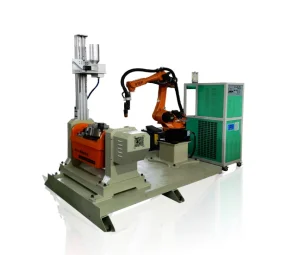
Integrating state-of-the-art Industry 4.0 automation, Chinese specialized PTA and laser cladding factories deliver standardized, highly reliable CNC gantry and robotic welding platforms. Factory-direct engineering ensures rapid production cycles without compromising build precision.
Equipment features internationally certified components including Siemens PLC control modules, Schneider electrical switchgear, customized high-precision powder feeders, and high-duty cycle cooling systems—offering long-term reliability for Grenville machine shops.
Every plasma surfacing system undergoes rigorous non-destructive testing (NDT), ultrasonic inspection, thermal stress mapping, and continuous 72-hour operational load tests prior to international dispatch to guarantee turnkey integration.
Customized Engineering Solutions Tailored for Critical Industry Components
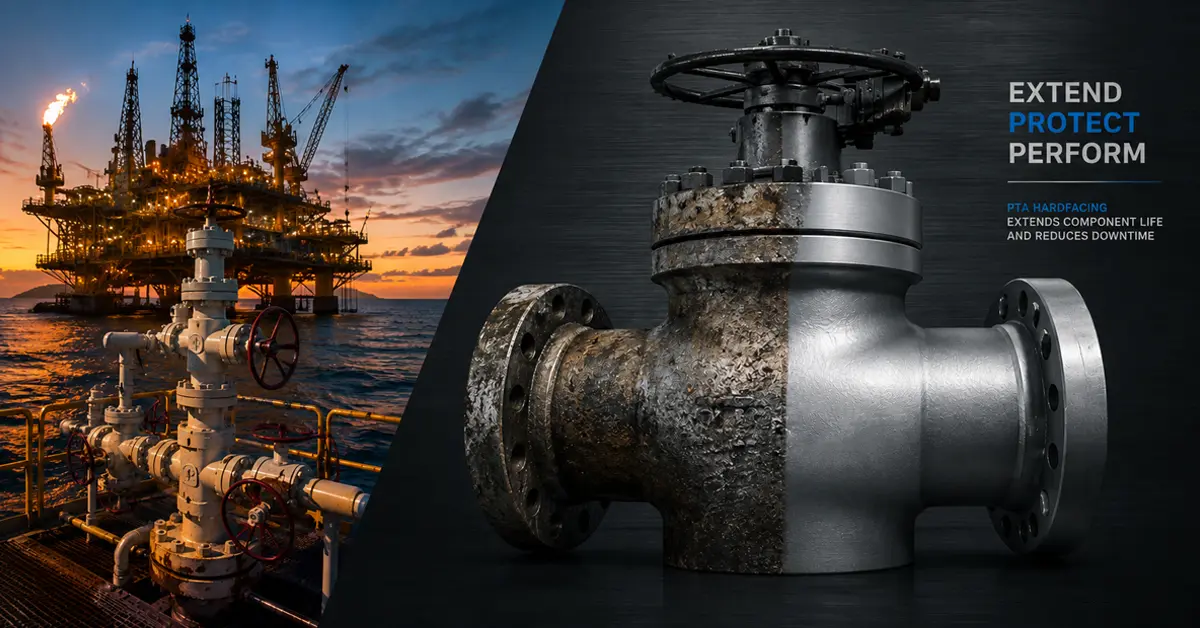
Grenville processing facilities handle erosive fluids, sand slurries, and high-pressure gas feeds. Components such as choke valve seats, gate valve discs, mud pump rods, and drill collar stabilizers require extreme surface hardness. PTA cladding deposits Stellite 6 or Tungsten Carbide alloys seamlessly, ensuring zero micro-fissures and extending operational longevity.
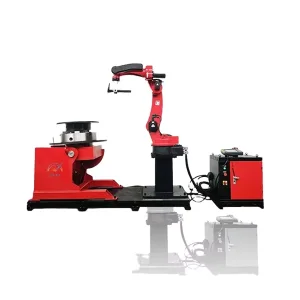
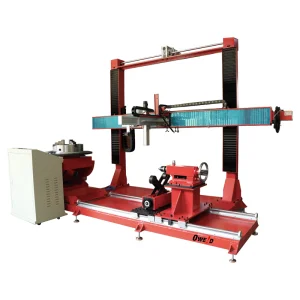
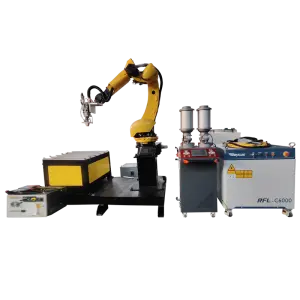
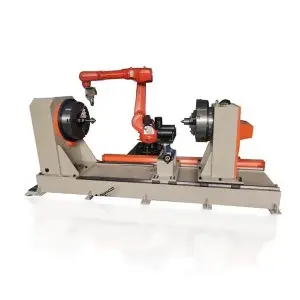
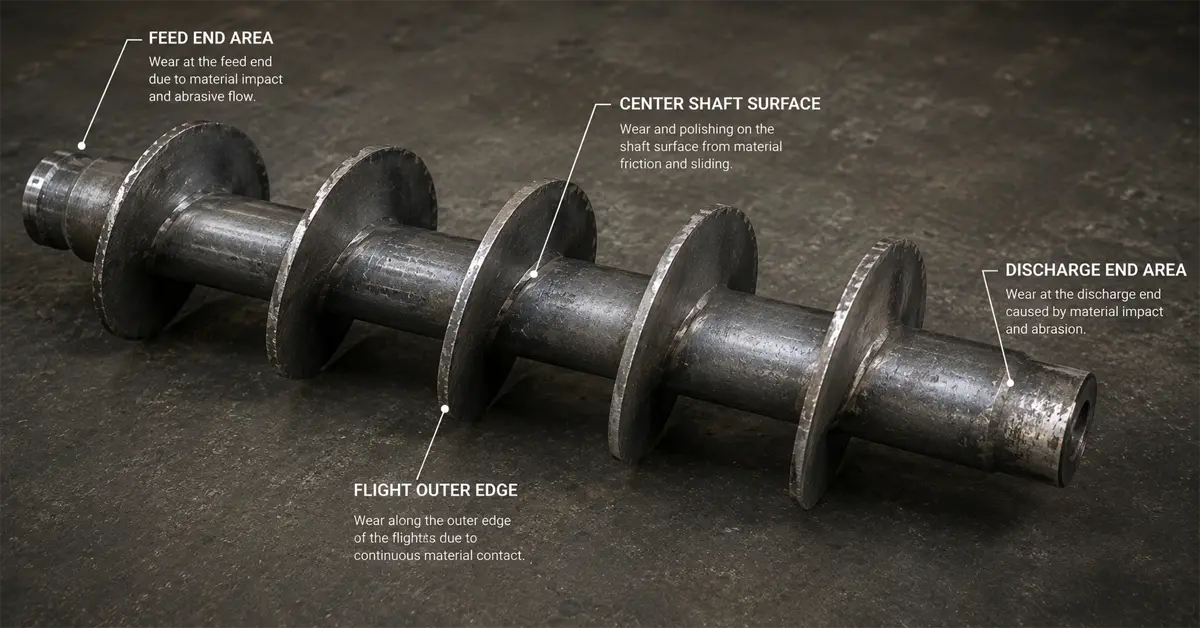
Severe earth abrasion damages conveyor screws, excavator teeth, slurry pump impellers, and hydraulic cylinder shafts. Utilizing automated multi-axis plasma surfacing systems (like the DYY-LC501), local maintenance crews rebuild lost material with iron-based or chromium-carbide hardfacing powders at a fraction of component replacement costs.
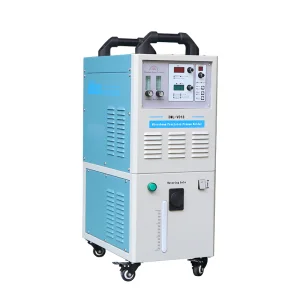
Micro plasma arc welding capabilities enable low-amperage precision repair on thin-walled aerospace housings, turbine blade edges, and heat exchanger diaphragms. The steady micro-arc starting prevents burn-through while guaranteeing micro-structural integrity.
Forging dies, hot-rolling mill rollers, and continuous casting molds suffer extreme thermal fatigue and cracking. Multi-functional robot plasma systems allow automated 3D overlay deposition to restore die geometry with high wear-resistant nickel-base superalloys.
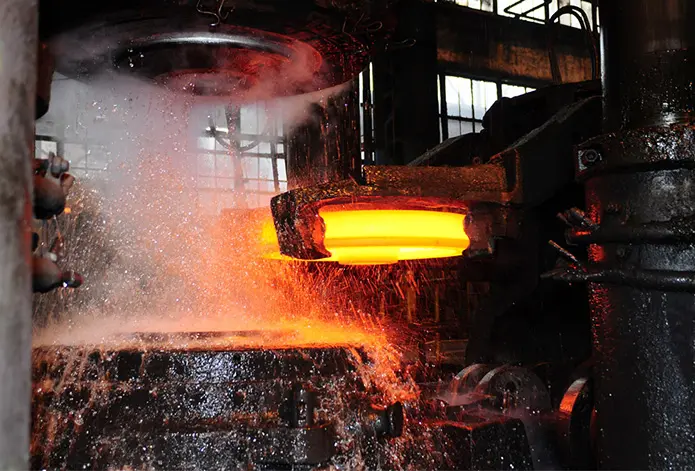
Explore Our Comprehensive Range of Precision Micro Arc, Automated Gantry, Laser Cladding, and Robotic Surfacing Systems
Shanghai Duomu has been a leading manufacturer and exporter of PTA cladding machines and laser cladding machines for more than ten years with a strong technical background and extensive international engineering experience.
We provide specialized automated cladding machinery, intelligent robotic workstations, and turnkey plasma surfacing solutions. Whether supplying industrial fabricators in Grenville or global machinery hubs, our mission centers on delivering defect-free deposition, reduced operational cost, and unprecedented machine longevity.
Get in Touch With Our Engineering DepartmentOur dedicated R&D department develops, produces, and tests plasma cladding equipment under ISO-9001 standards. The equipment maintains efficient long-term operation under heavy continuous duty cycles in high-temperature environments.
In addition, our automated laser cladding systems effectively support large-scale remanufacturing projects. We deliver custom solutions including hydraulic rod cladding equipment, coal mining pick cladding machines, automatic ball valve overlay stations, and customized plasma bore torches.
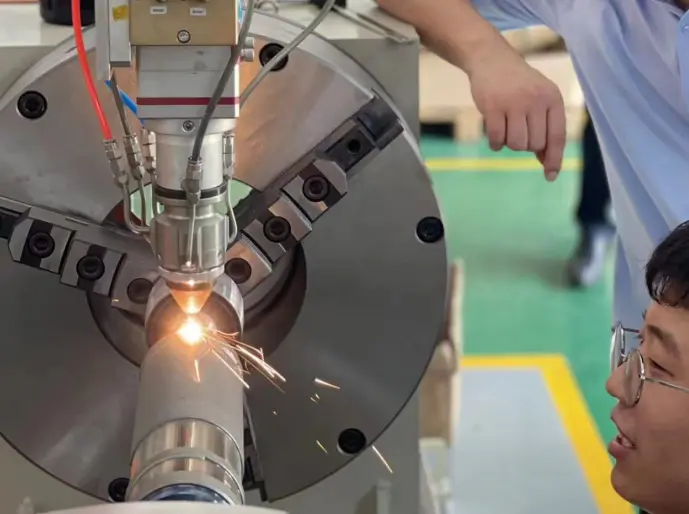
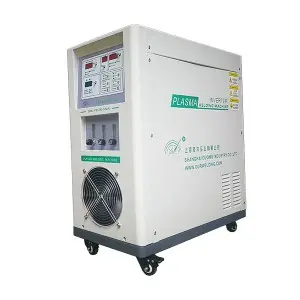
Expert Technical Knowledge on Dilution Control, Downtime Reduction, and Metallurgical Bond Strength
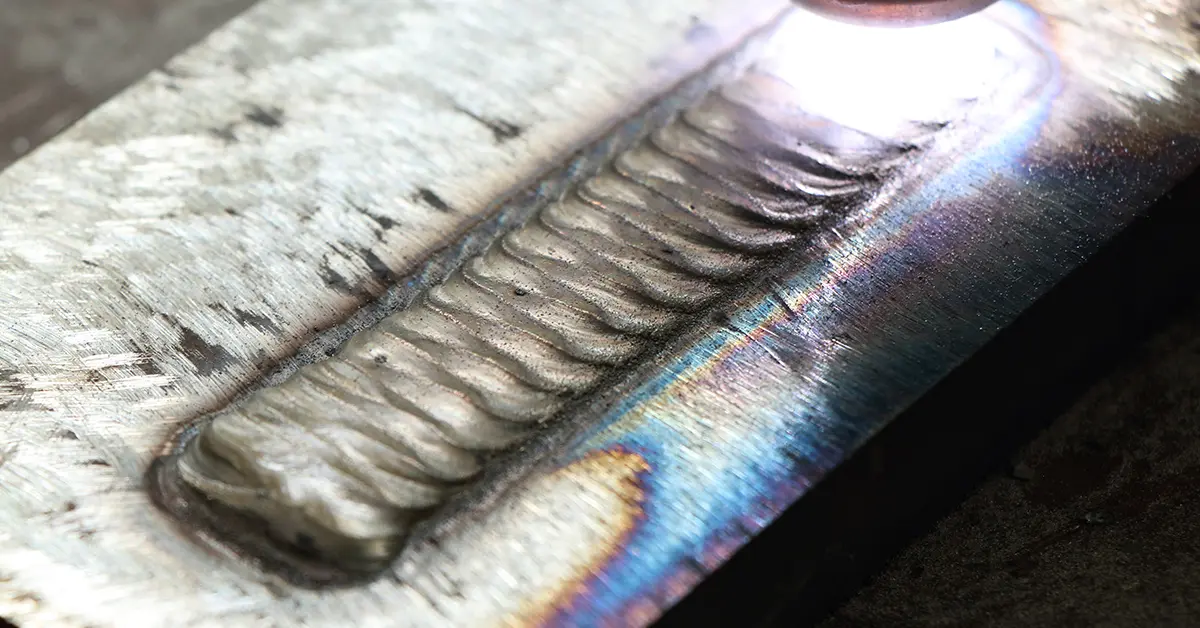
"In Plasma Transferred Arc (PTA) hardfacing, achieving a high-quality overlay is not only about selecting the right alloy powder or optimizing welding parameters. One of the most critical factors that directly affects overlay performance is the dilution rate. By maintaining dilution under 5%, full hardness is achieved in a single pass."
"In Oil & Gas, the real cost is downtime—not the component. When a choke valve fails due to sand erosion or a mud pump valve seat wears beyond tolerance, PTA cladding restores geometry with Cobalt Stellite alloys, increasing service life by over 400% in Grenville installations."
"In mining, cement, and power generation, screw conveyors and wear plates are key causes of unplanned downtime. Automated plasma surfacing applies uniform chromium carbide layers, drastically reducing mechanical friction and structural abrasion."
Technical Guidance on Plasma Transferred Arc Procurement, Logistics, and Operation in Grenville